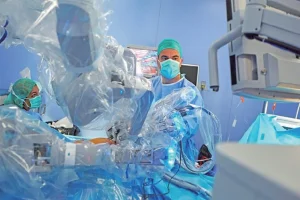
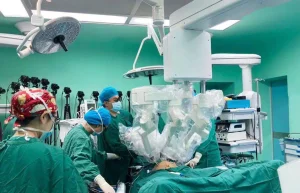
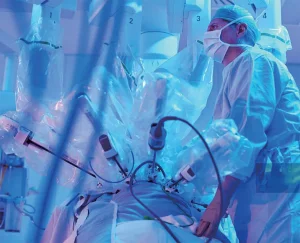
Premium medical device drapes and protective systems optimized for immediate deployment within surgical suites, clinical labs, and emergency care environments.


An in-depth evaluation of infection control protocols, hospital operating constraints, and sterile barrier demands in Cameroon's Northwest Region.
The healthcare infrastructure within Bamenda and the broader Northwest Region of Cameroon is undergoing a vital transformation. Major hospital structures, including regional hospitals and faith-based medical centers, face dual pressures: managing high patient turnarounds while ensuring strict adherence to global infection mitigation guidelines. Operating rooms require continuous sterile integrity to prevent surgical site infections (SSIs), which can severely compromise surgical outcomes and escalate operational overheads.
Environmental conditions such as ambient humidity levels and varying particulate profiles require reliable protection for high-value diagnostic systems and operating machinery. Unprotected medical instruments—including surgical microscopes, mobile C-arms, and flexible endoscopes—are vulnerable to persistent fluids and biological contaminants. Deploying targeted, single-use technical protective drapes ensures continuous safety compliance during both routine and complex operations.
Acquiring reliable medical supplies for healthcare operations across Bamenda demands a resilient logistical framework. Shipments generally enter via the commercial transport hub at Douala Port before moving inland through key transit routes to the Northwest territory. This distance necessitates highly resilient, space-efficient protective packaging capable of withstanding physical stress and moisture changes.
E-E-A-T Technical Framework Note: Every sterile protective shield deployed to the Bamenda sector is processed under standardized Ethylene Oxide (EO) sterilization sequences, verified with integrated chemical tracking monitors, and enclosed within high-resistance puncture-proof medical pouches to guarantee zero-loss sterility upon opening.
A rigorous examination of polymer formulations, lens integration tech, and puncture resistance metrics required for critical medical equipment covers.
Our industrial production facilities utilize custom low-density and linear low-density polyethylene (LDPE/LLDPE) blown film formulations. These polymers are optimized to maximize multi-directional tear strength and prevent sudden micro-punctures during adjustment of surgical arms and articulating brackets.
The material remains highly pliable and soft to touch, minimizing operational friction noise within clinical suites, while maintaining an unyielding viral and liquid block profile meeting rigorous ISO standards.
For specialized equipment like Zeiss and Leica operating microscopes or precision endoscopic instrumentation, maintaining crisp visibility is critical. Our covers incorporate optical-grade, anti-reflective, scratch-resistant copolyester lenses.
These components are mechanically heat-sealed to the surrounding film barriers within clear, high-frequency induction zones to eliminate optical distortion, ensuring uninterrupted clarity during fine micro-surgical techniques.
To secure draping solutions over rapidly moving or vibrating clinical machines, specialized skin-safe, residue-free medical acrylic adhesives are precisely applied. These tape points allow fast setup cycles by nursing personnel while holding firm under considerable load stress and fluid contact, without leaving any sticky residue on delicate electronics when removed.
Leveraging specialized technical execution, automated manufacturing, and rigorous quality systems to build global healthcare trust.
Founded with a strong commitment to the healthcare industry, Hebei ROA Medicare Co., Ltd. has been dedicated to providing high-quality medical and healthcare products to customers worldwide. Over the years, we have consistently upheld the belief that “Health, Trust, and Innovation are the foundation of every family and society.” Driven by this philosophy, ROA Medicare has grown into a professional and reliable supplier in the global healthcare market, continuously improving product quality, expanding international cooperation, and contributing to better healthcare solutions for people around the world.
The name “ROA Medicare” represents responsibility, professionalism, and care for human health. We believe that healthcare is not only about products, but also about trust, safety, and long-term commitment to customers and patients worldwide. Our company logo and brand identity reflect our dedication to the medical industry. The combination of blue and green symbolizes professionalism, reliability, health, and vitality. Blue represents safety, precision, and trustworthiness, while green reflects life, healing, sustainability, and hope. Together, they embody our mission to deliver safe and effective medical products that improve quality of life.
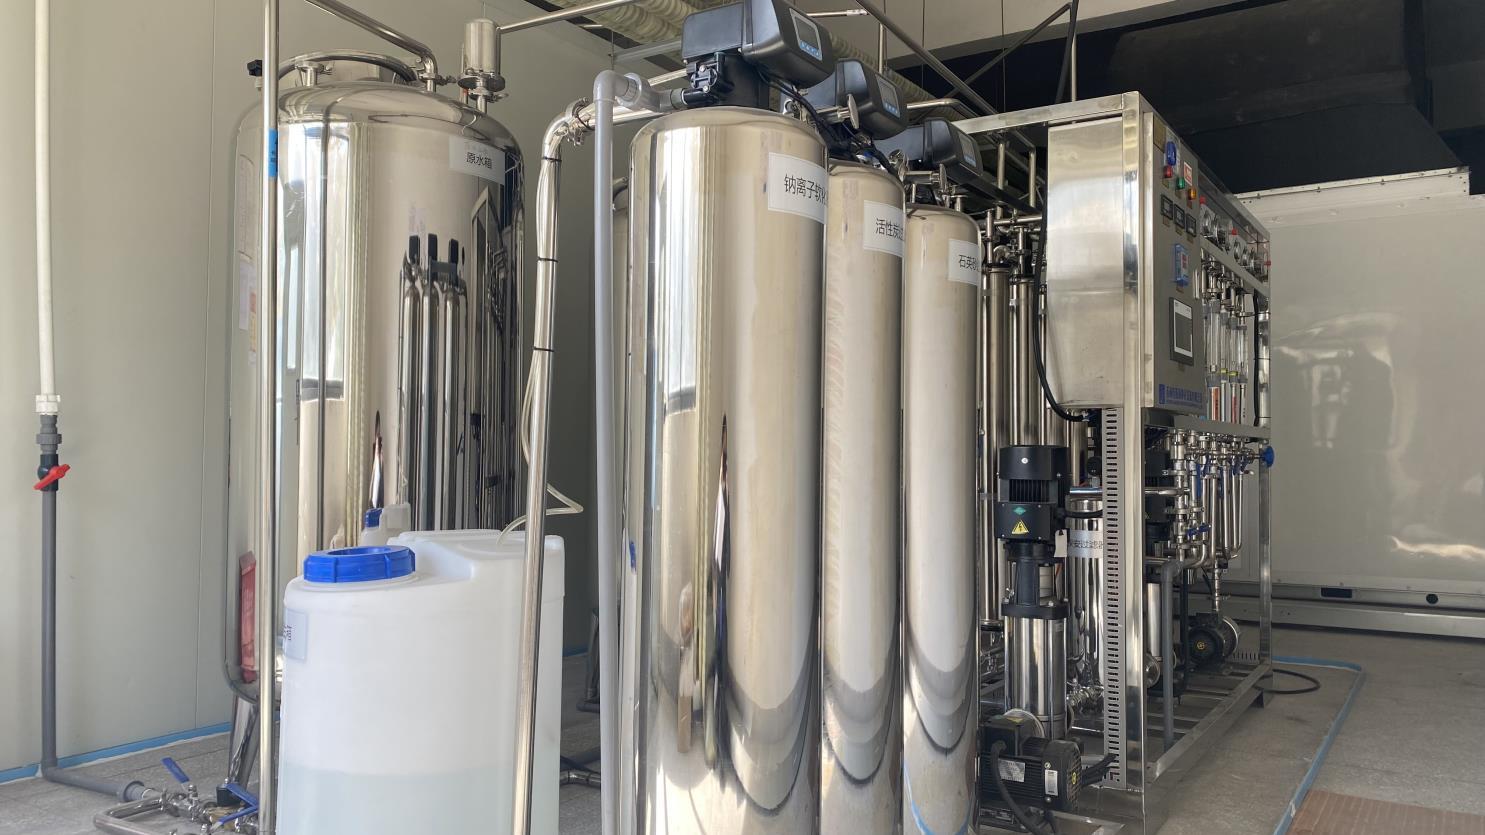
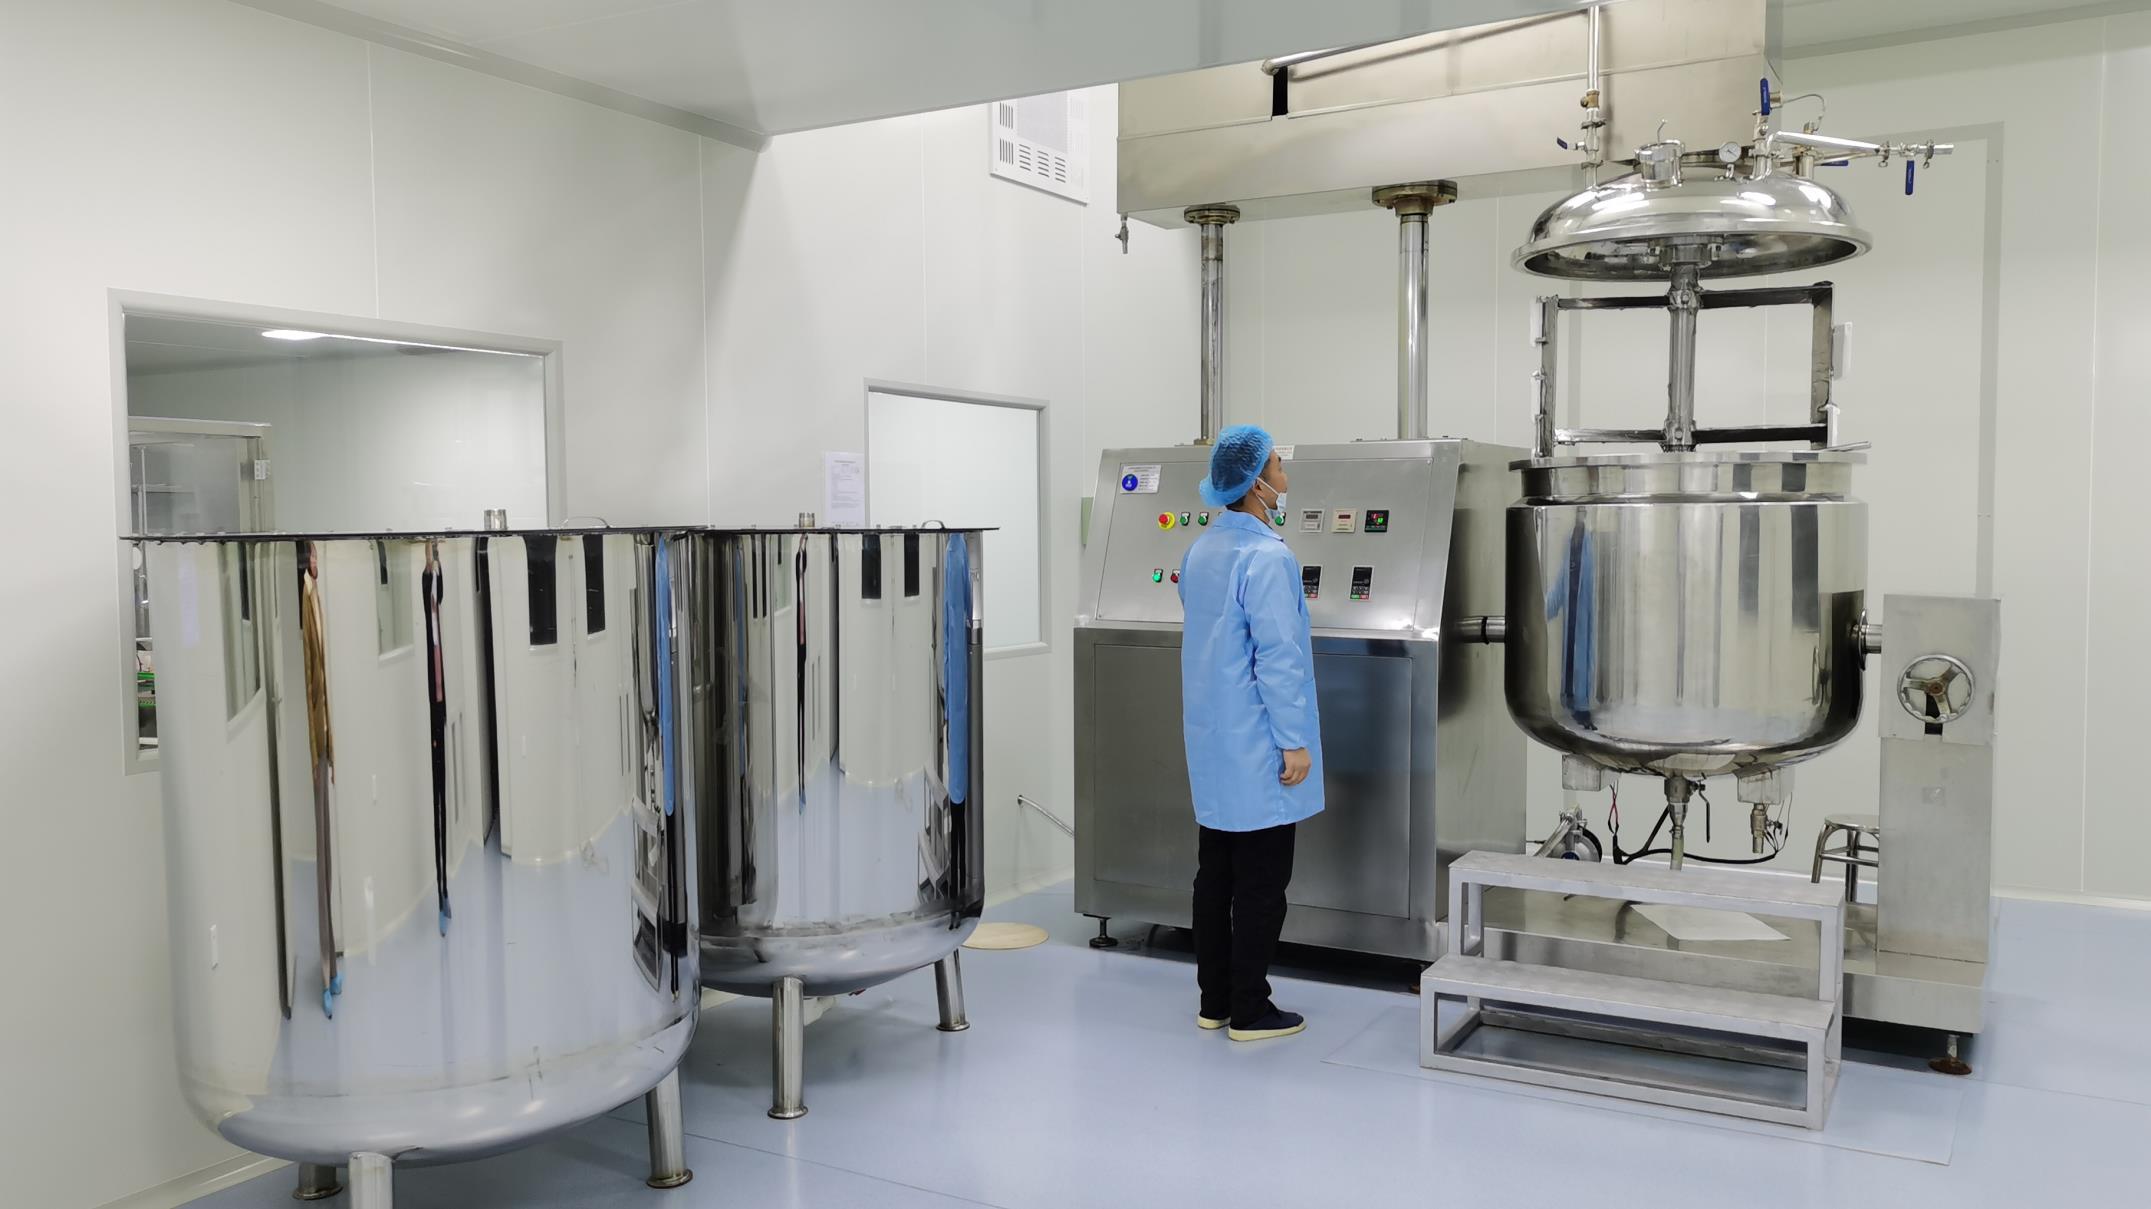
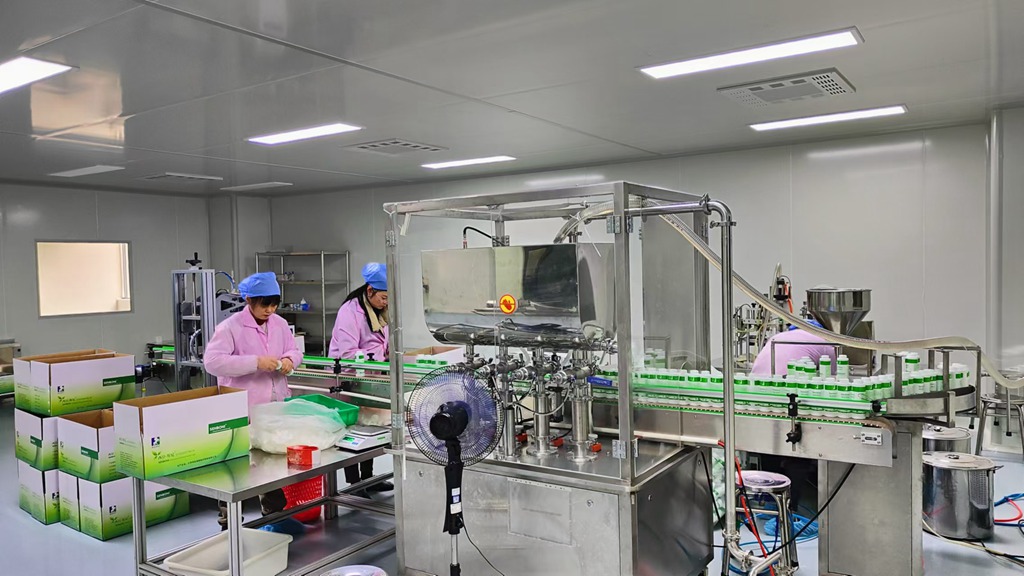
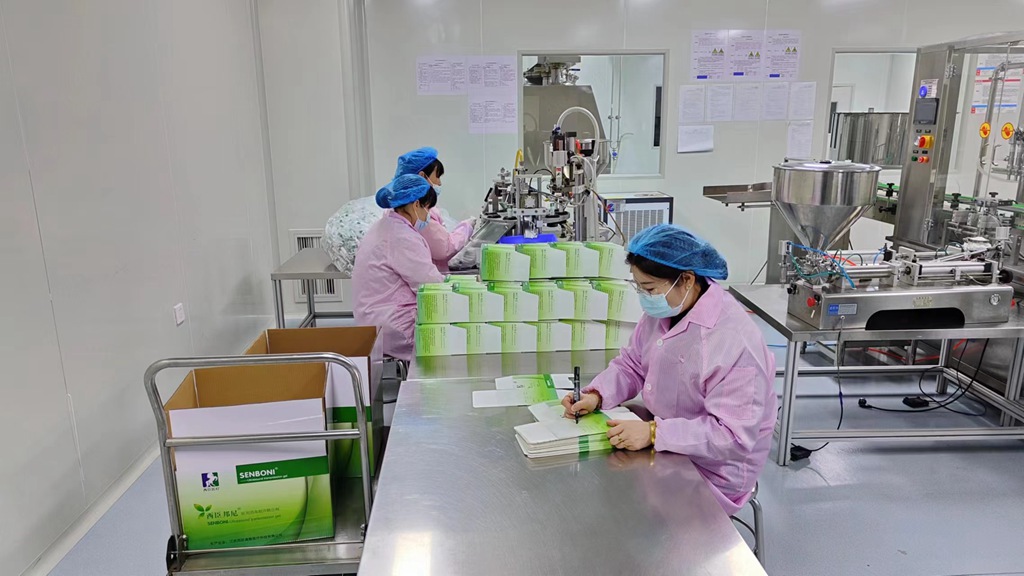
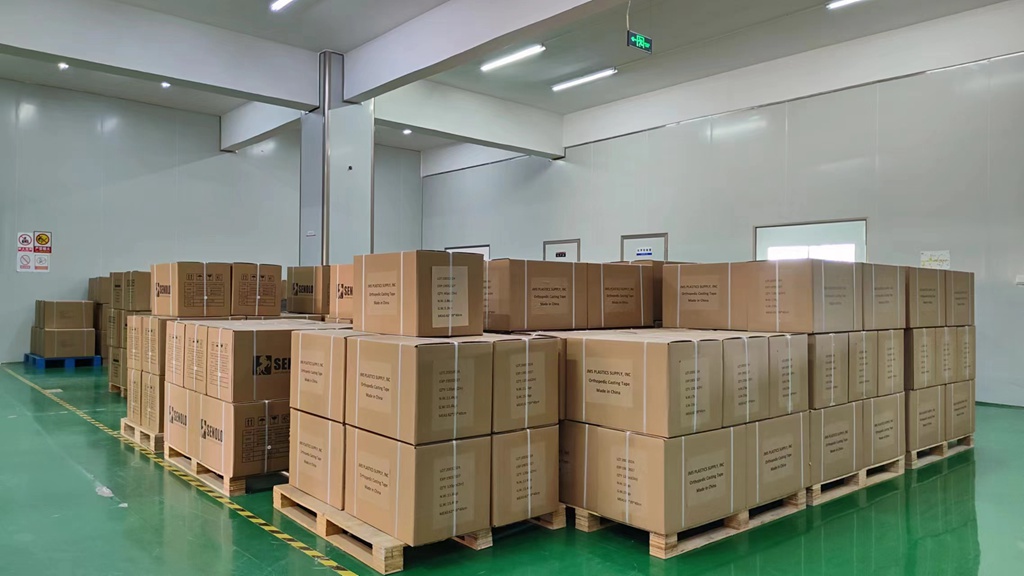
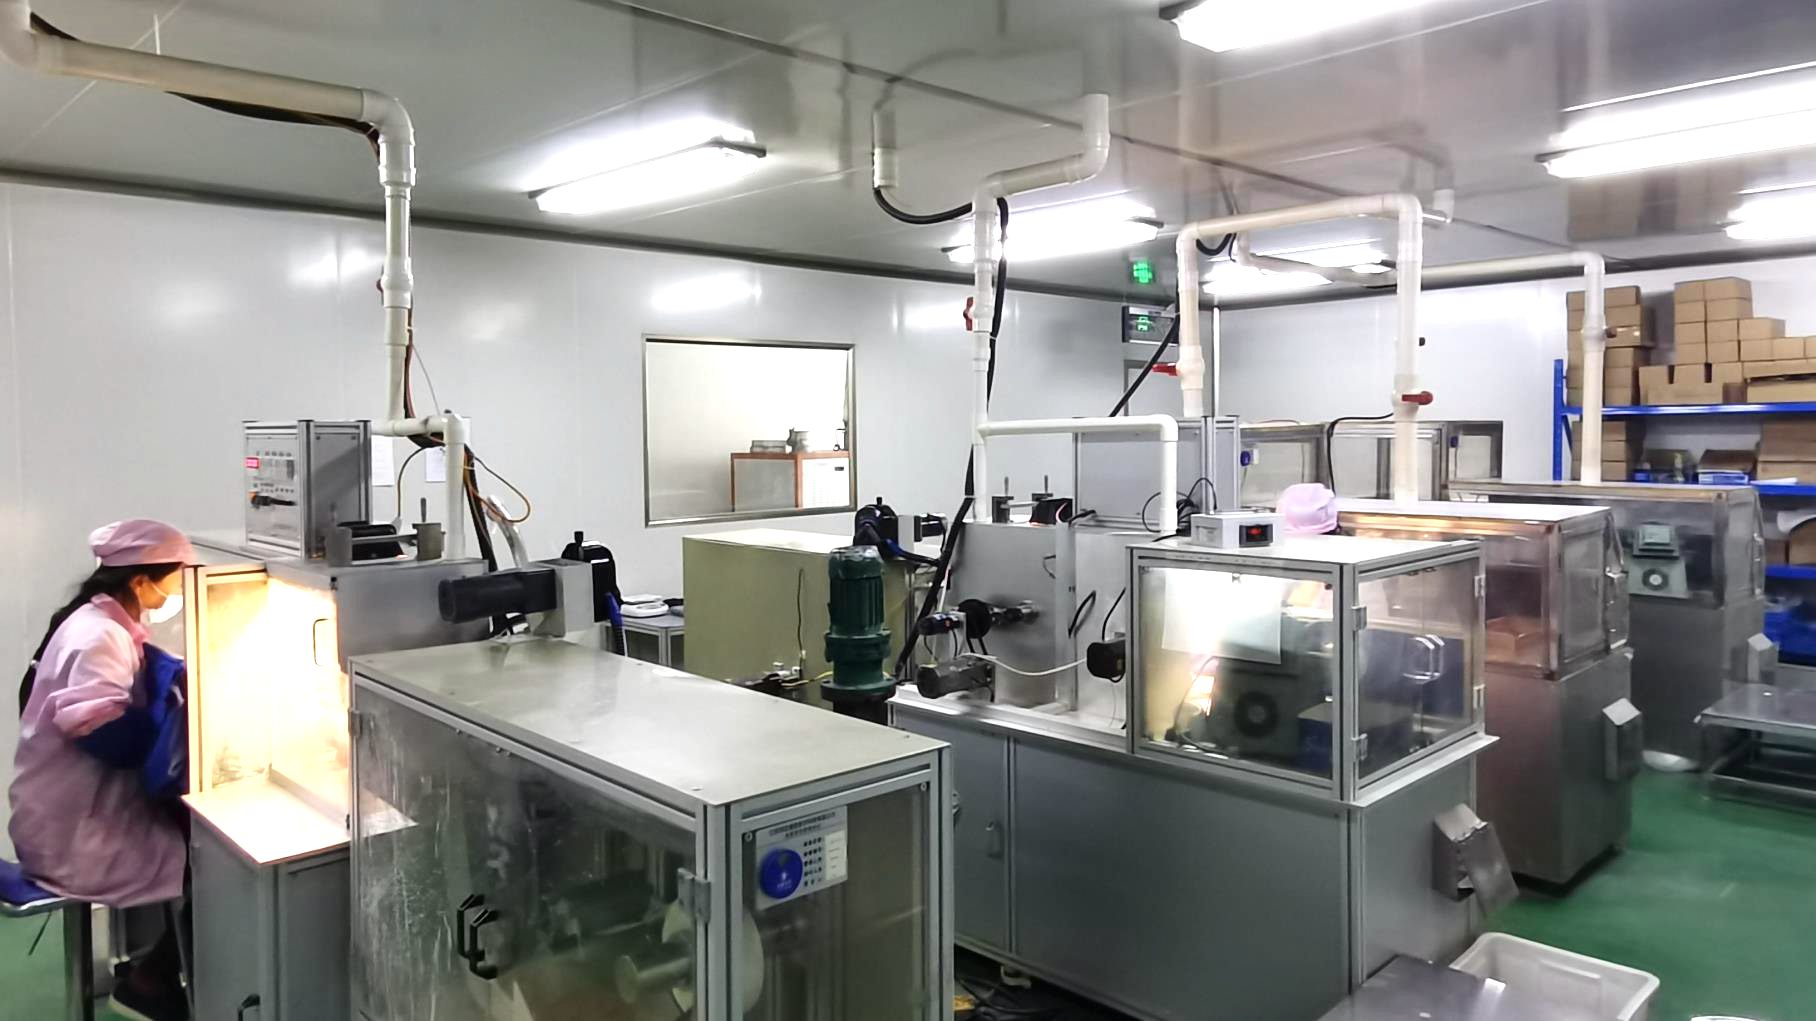
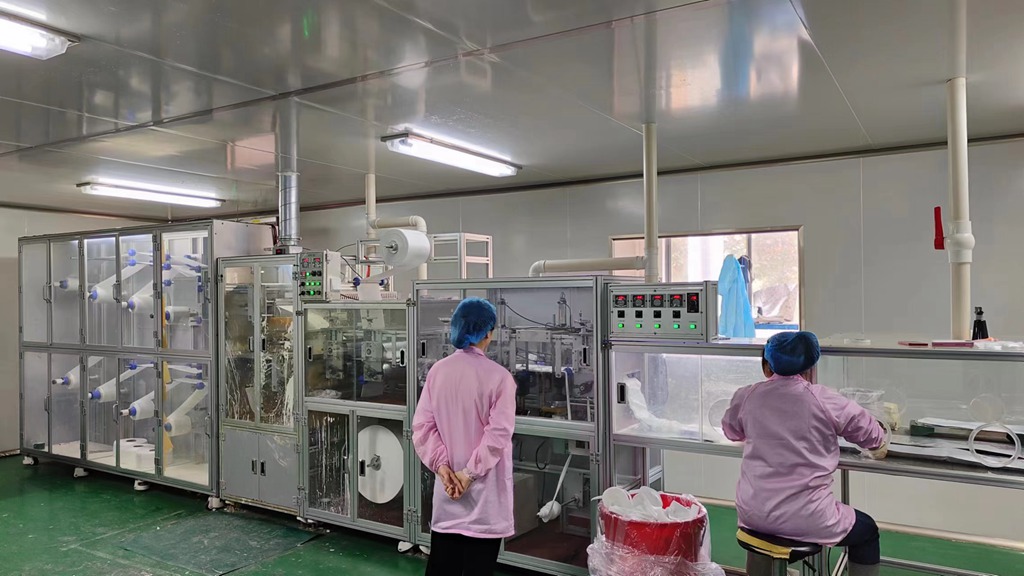
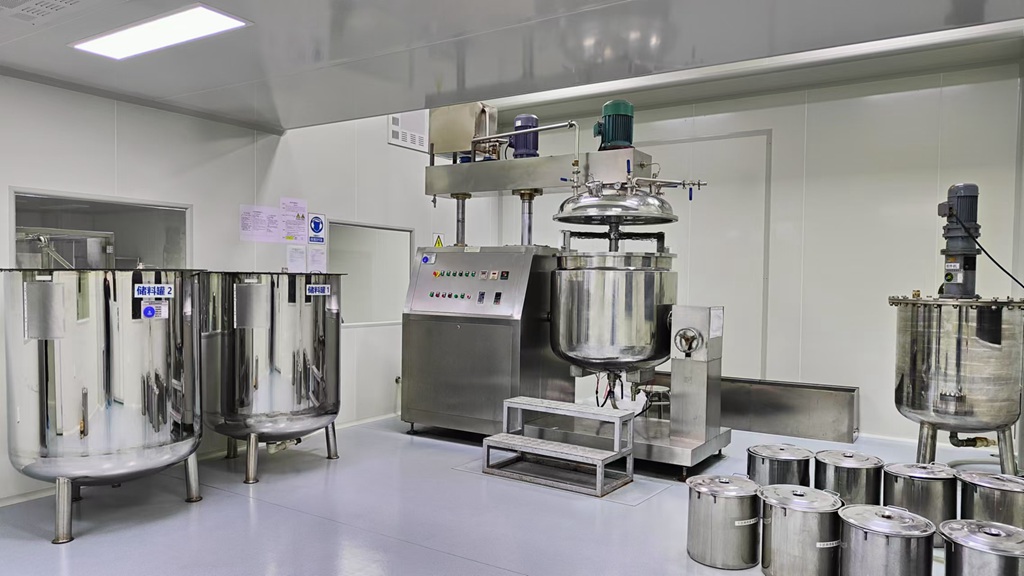
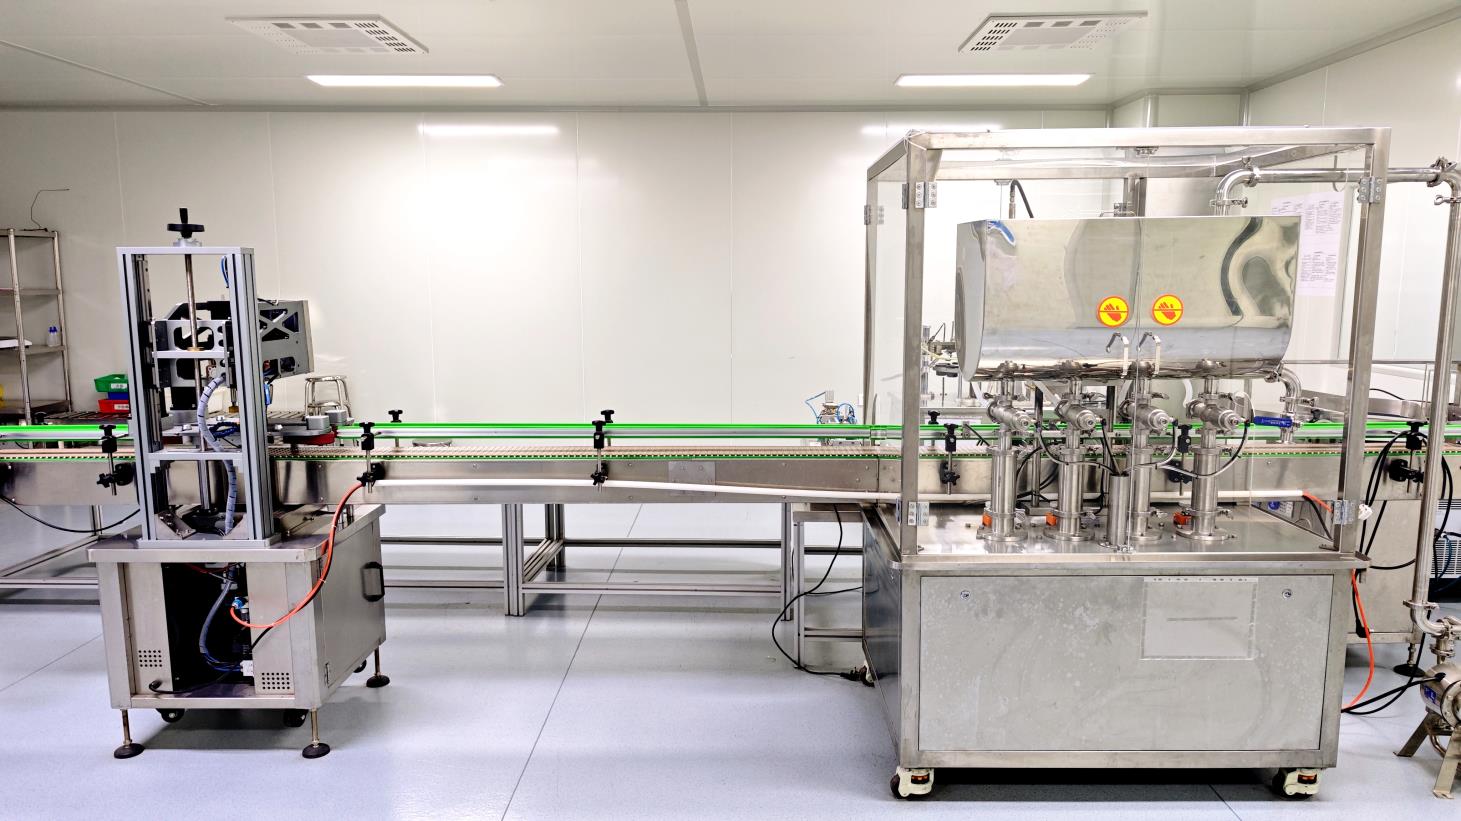
At ROA Medicare, we understand that every protective cover we manufacture and every service we provide directly impacts human health and well-being. Therefore, we strictly follow international quality management standards and continuously improve our manufacturing and inspection systems to ensure product safety and reliability. Through continuous innovation and professional service, we aim to meet the evolving demands of the global healthcare industry.
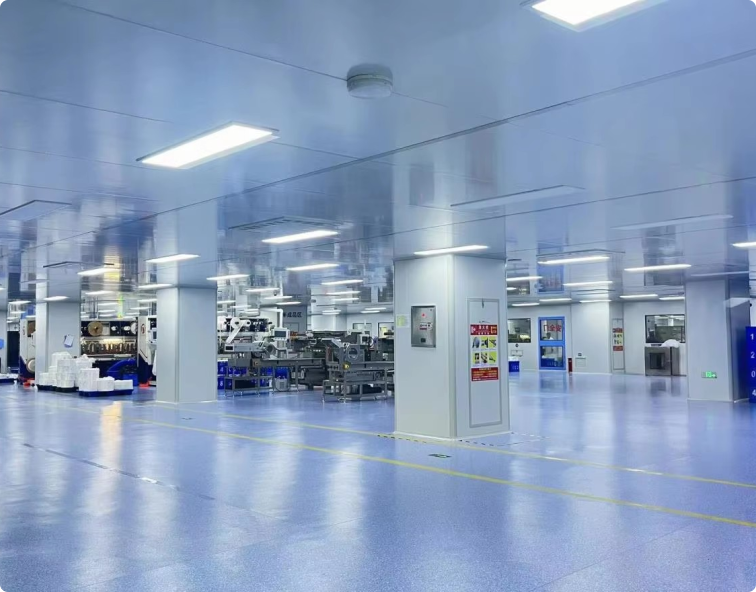
How Hebei ROA Medicare balances high-capacity supply chain agility with stringent green manufacturing and regulatory compliance.
ROA Medicare specializes in a wide range of medical and healthcare products, including medical disposables, hospital equipment, homecare products, rehabilitation supplies, diagnostic systems, and specialized surgical and protective products. Our products are exported to Europe, America, the Middle East, Africa, Southeast Asia, and many other international markets. With stable product quality, competitive pricing, and professional service, we have established long-term cooperative relationships with healthcare facilities worldwide.
Environmental protection and sustainable development are core pillars of ROA Medicare's long-term strategy. We actively promote green development through environmentally friendly polymer choices, energy-saving production processes, waste reduction, resource optimization, and sustainable supply chain management. We strive to reduce our environmental footprint while continuously delivering safe, innovative healthcare products to the global market.
For distributors serving regional African medical networks, supply chain delays can interrupt clinical schedules. We address this by maintaining deep buffer stocks of raw materials and optimizing packaging to lower volumetric shipping rates. Our shipping documentation accommodates targeted inspection requirements, ensuring swift validation through customs clearance structures at regional transit hubs like Douala and seamless final delivery into Bamenda.
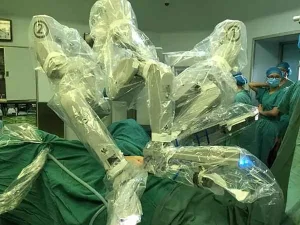
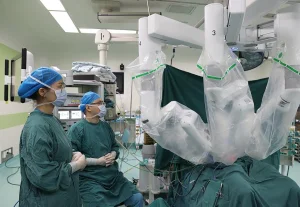
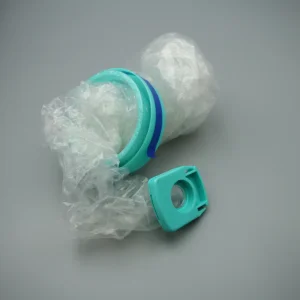
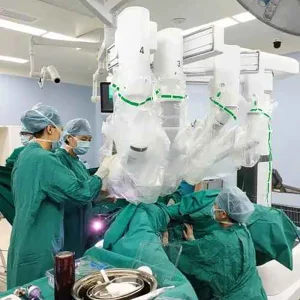
Browse our complete catalog of specialized equipment drapes, robotic arm systems, and diagnostic instrument covers designed for sterile clinical preservation.



Expert clarifications regarding testing methodologies, product customizability, minimum order configurations, and delivery pathways for regional African buyers.
 ROA Medicare