Explore our precision-engineered healthcare consumables, medical-grade components, and specialized equipment certified for worldwide clinical deployment.
The global medical device and patient care manufacturing ecosystem is undergoing a structural transformation driven by an aging demographic, the expansion of post-acute home healthcare, and stringent international compliance frameworks such as EU MDR (2017/745) and US FDA 21 CFR Part 820. As hospitals and outpatient clinical networks demand higher biocompatibility, sterility assurance, and customized mechanical configurations, selecting an experienced OEM/ODM contract manufacturer has become a pivotal strategic imperative.
Hebei ROA Medicare Co., Ltd. stands at the convergence of advanced material science, automated medical plastic processing, and full lifecycle contract manufacturing. We empower original equipment manufacturers (OEMs), international hospital supply distributors, and pharmaceutical brand owners to accelerate market entry, optimize unit costs, and uphold uncompromised patient safety across diverse clinical applications.
Founded with a strong commitment to the healthcare industry, Hebei ROA Medicare Co., Ltd. has been dedicated to providing high-quality medical and healthcare products to customers worldwide. Over the years, we have consistently upheld the belief that "Health, Trust, and Innovation are the foundation of every family and society."
Driven by this philosophy, ROA Medicare has grown into a professional and reliable supplier in the global healthcare market, continuously improving product quality, expanding international cooperation, and contributing to better healthcare solutions for people around the world.
The name "ROA Medicare" represents responsibility, professionalism, and care for human health. We believe that healthcare is not only about manufacturing products, but also about cultivating trust, engineering absolute clinical safety, and maintaining a long-term commitment to hospital procurement directors, clinical specialists, and homecare users worldwide.
Our corporate identity reflects our systemic dedication to the medical industry. The strategic combination of blue and green symbolizes technical precision, biological reliability, health, and vitality. Blue represents cleanroom safety, regulatory rigor, and structural trustworthiness, while green reflects organic life, patient recovery, environmental sustainability, and hope. Together, they embody our corporate mission to deliver safe, compliant, and highly effective medical devices.
At ROA Medicare, we understand that every product we manufacture and every engineering service we execute directly impacts clinical outcomes and human well-being. Therefore, we rigidly adhere to our foundational principle:
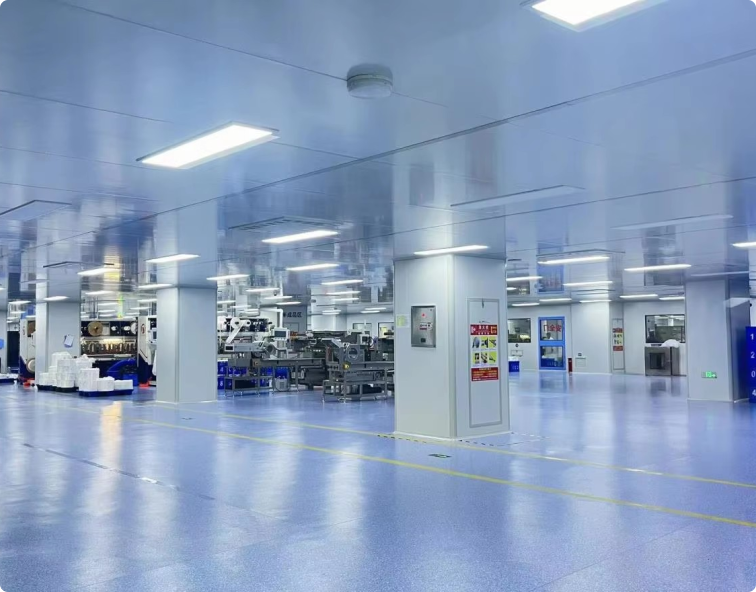
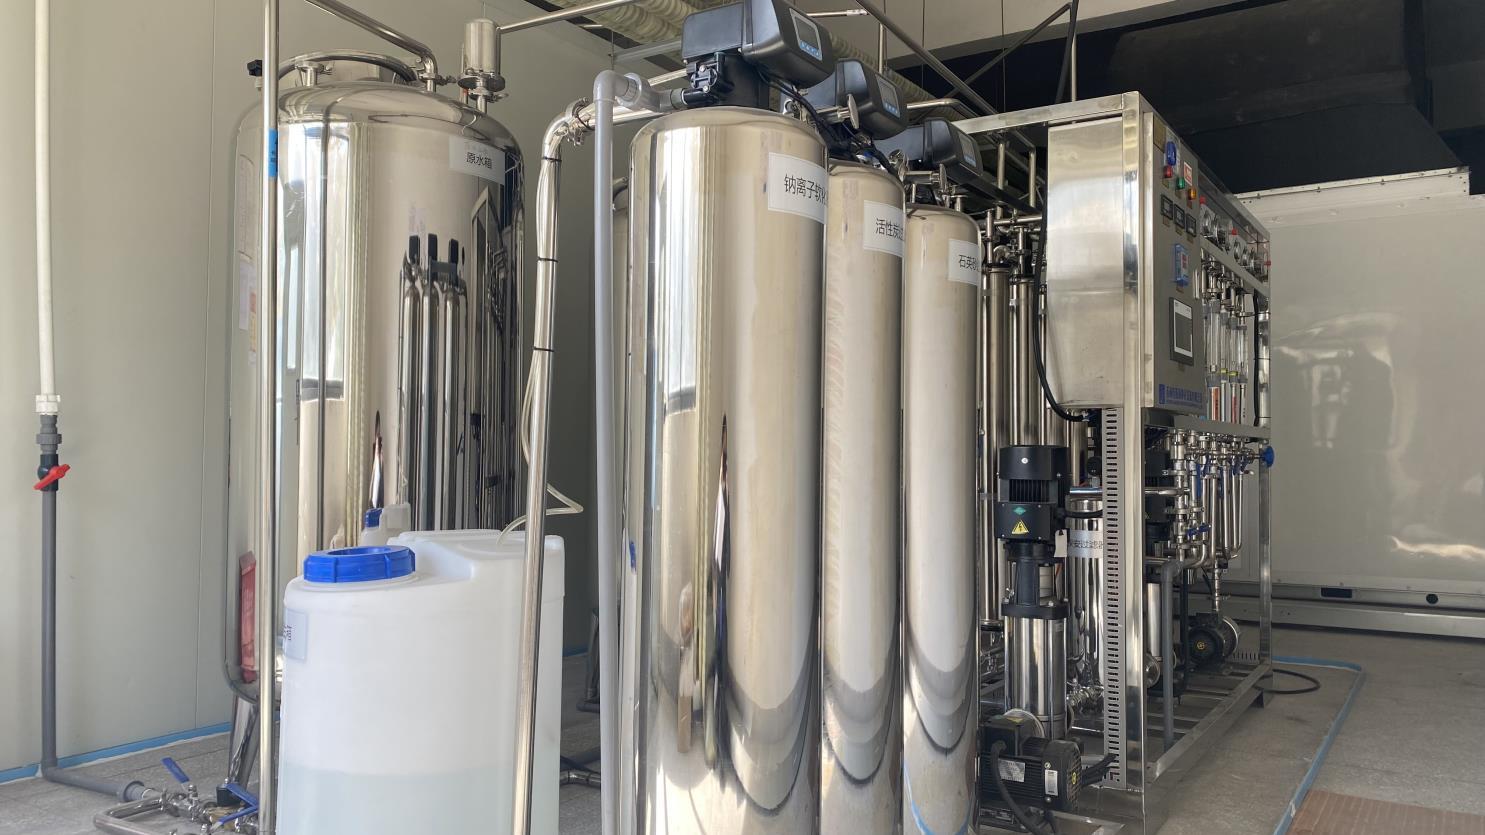
To deliver zero-defect patient care devices and OEM customized medical components, Hebei ROA Medicare Co., Ltd. operates state-of-the-art production floors equipped with automated fluid purifiers, high-precision mixing units, cleanroom liquid filling lines, automated casting tape processing, and climate-controlled warehousing.
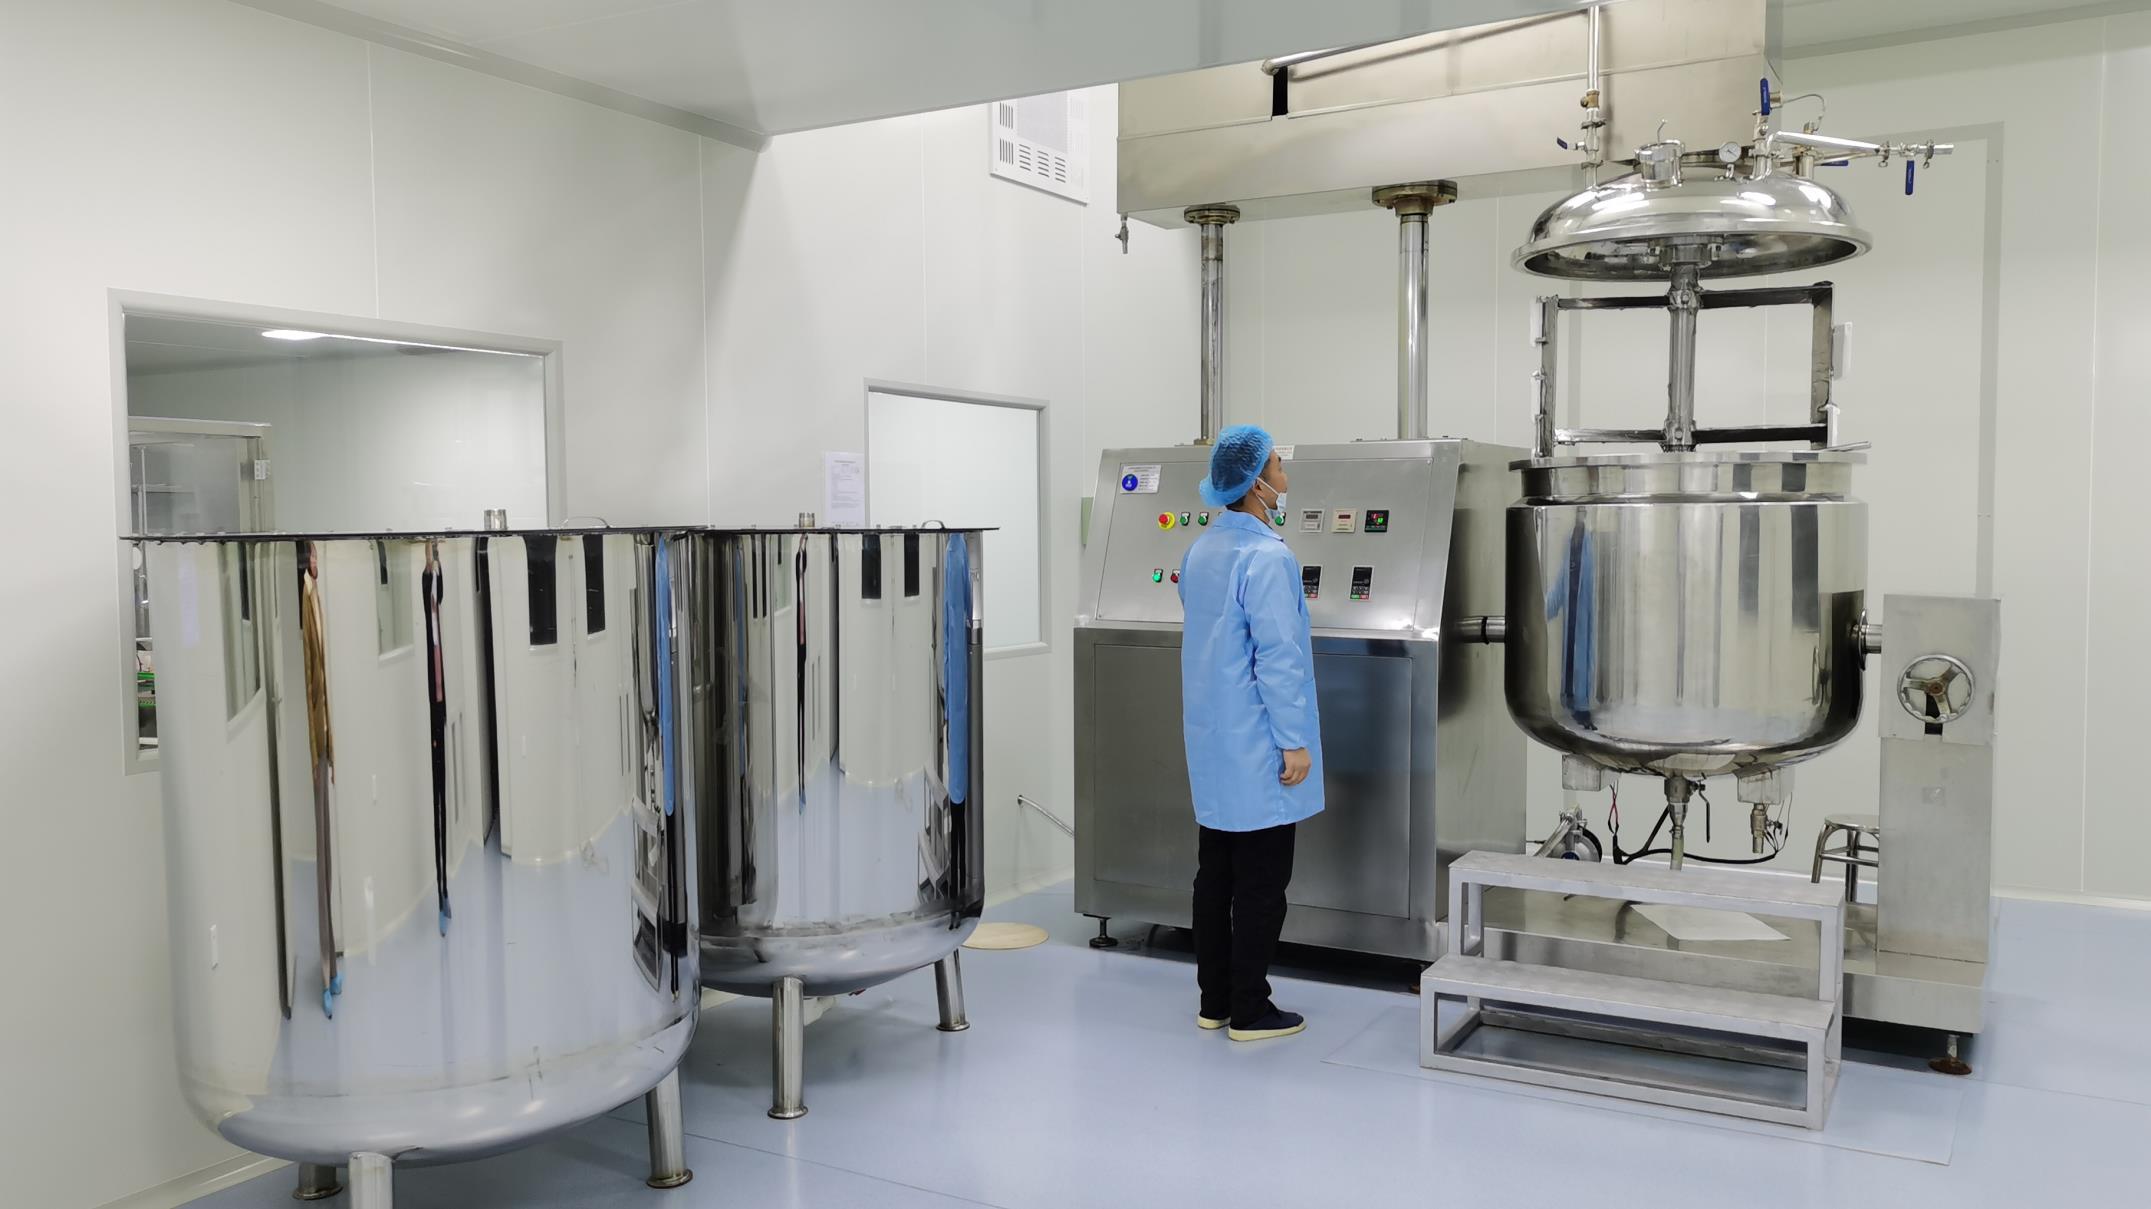
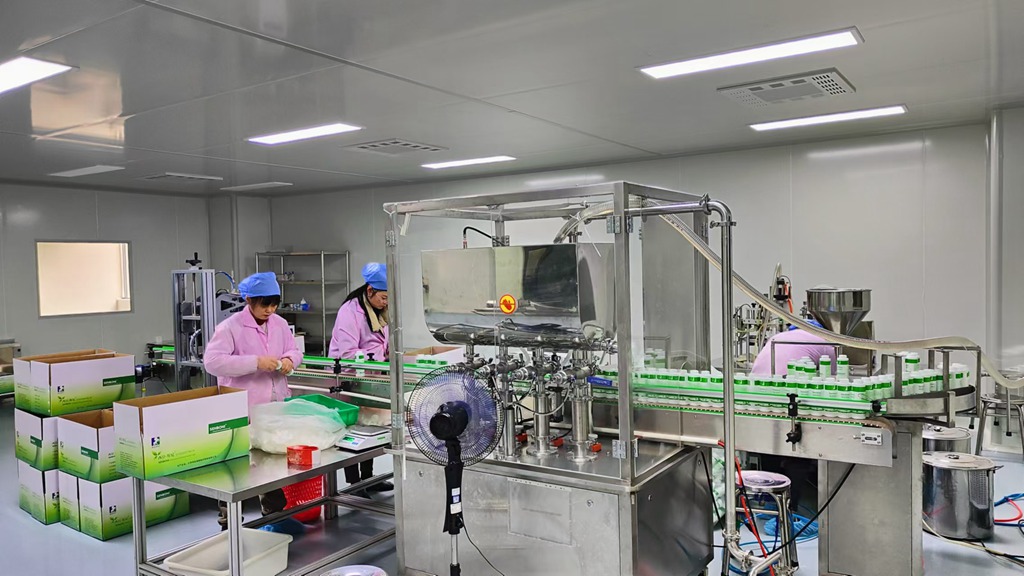
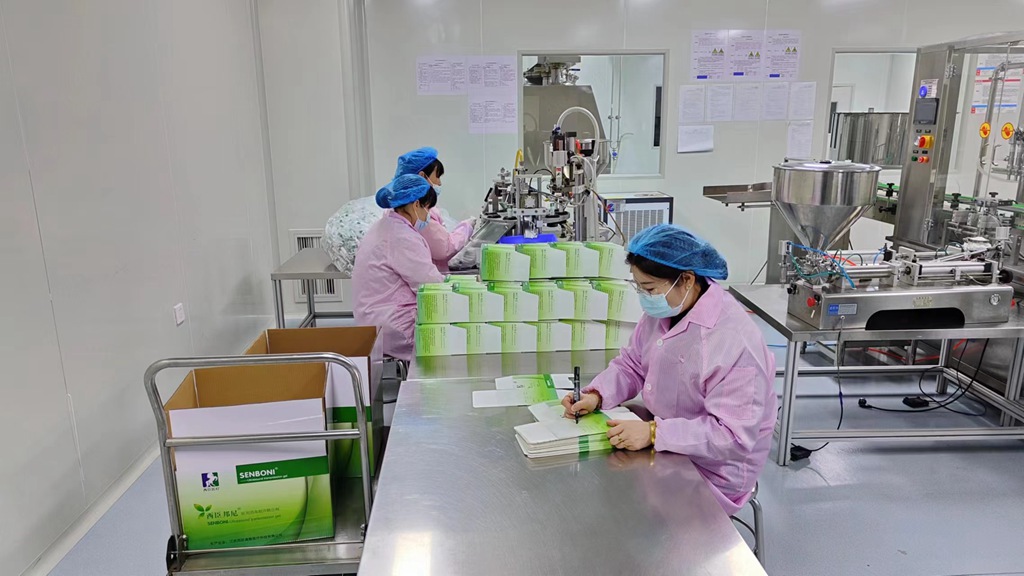
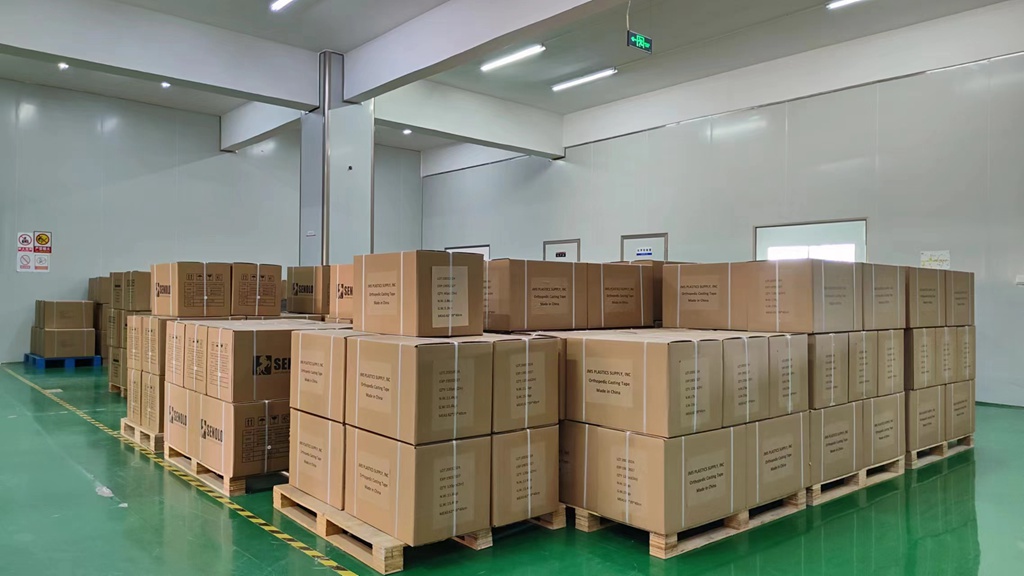
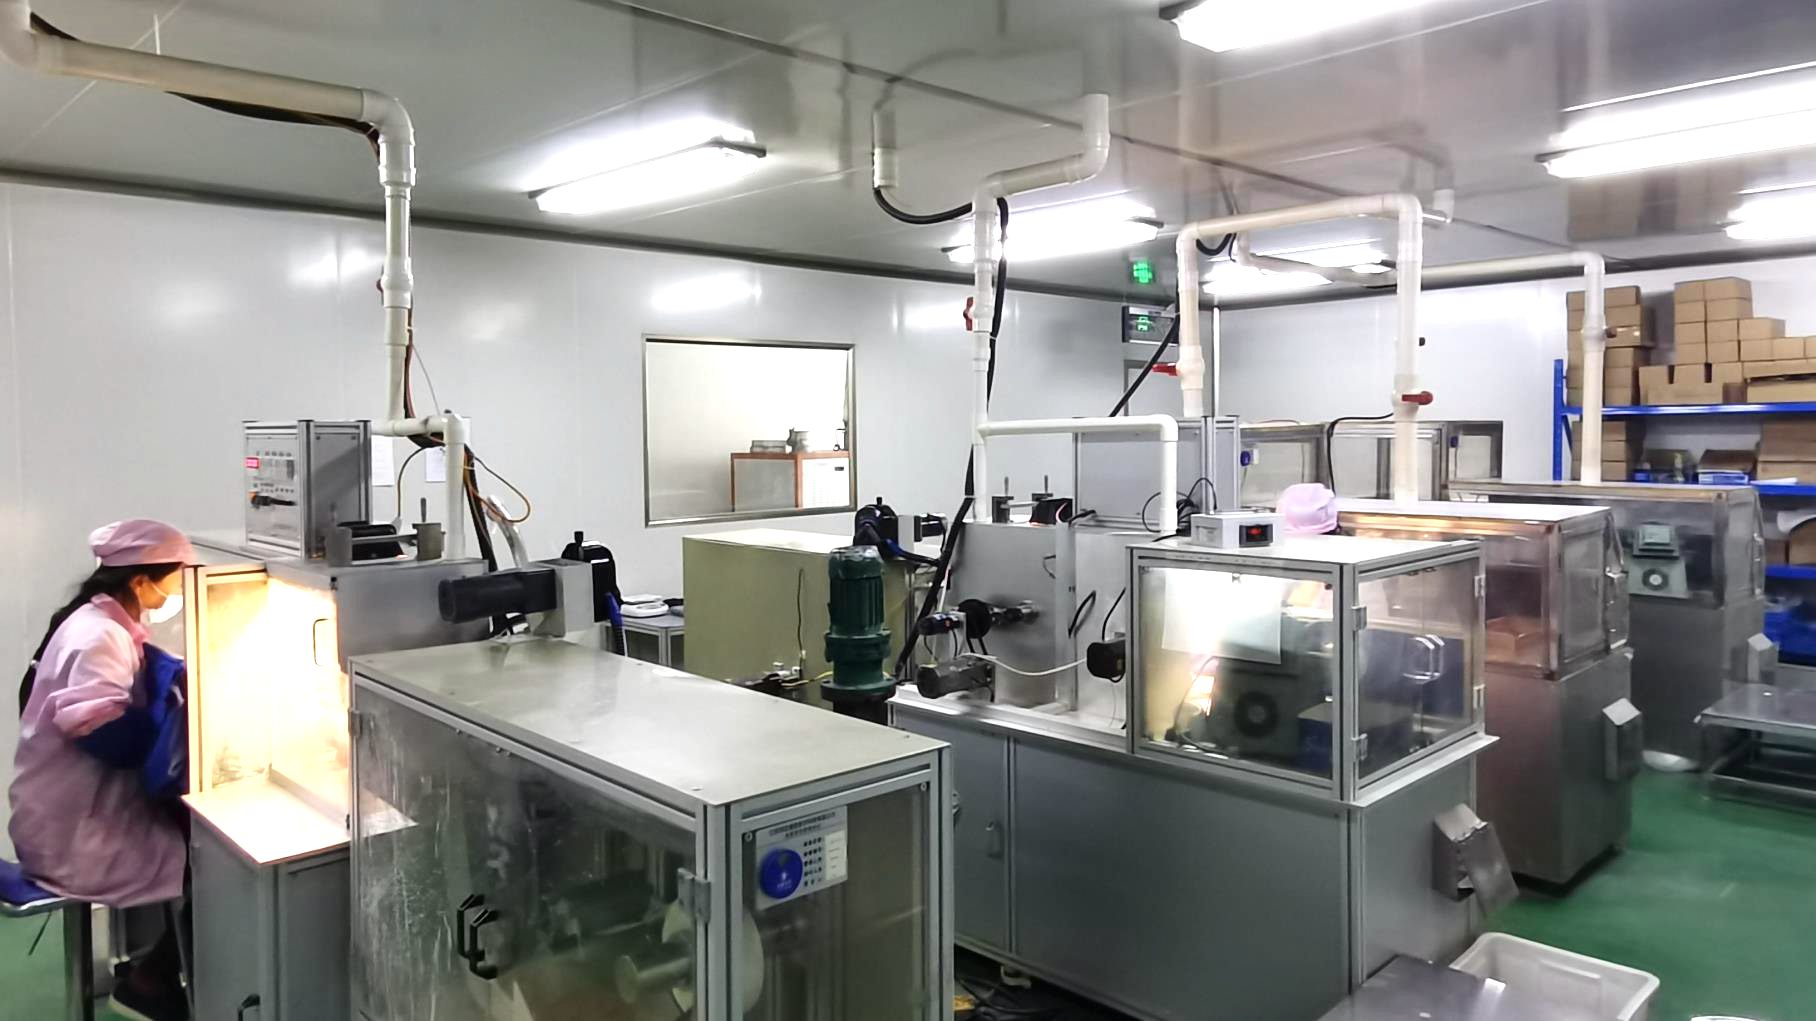
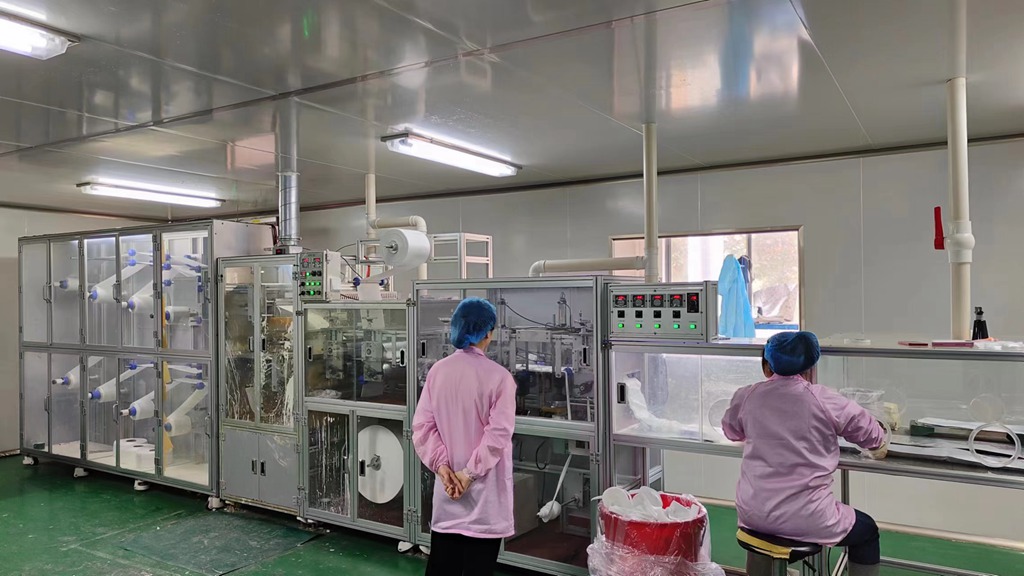
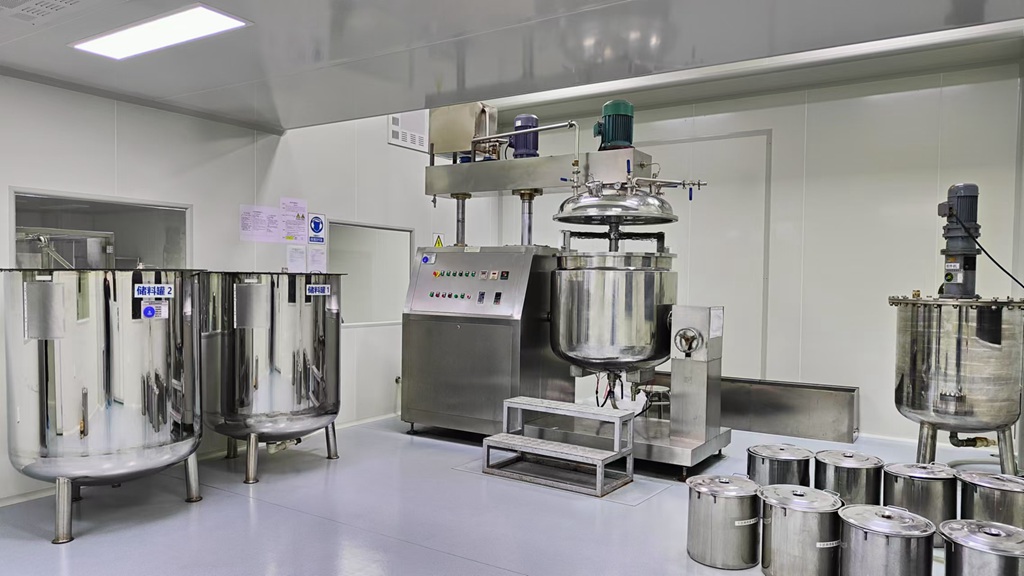
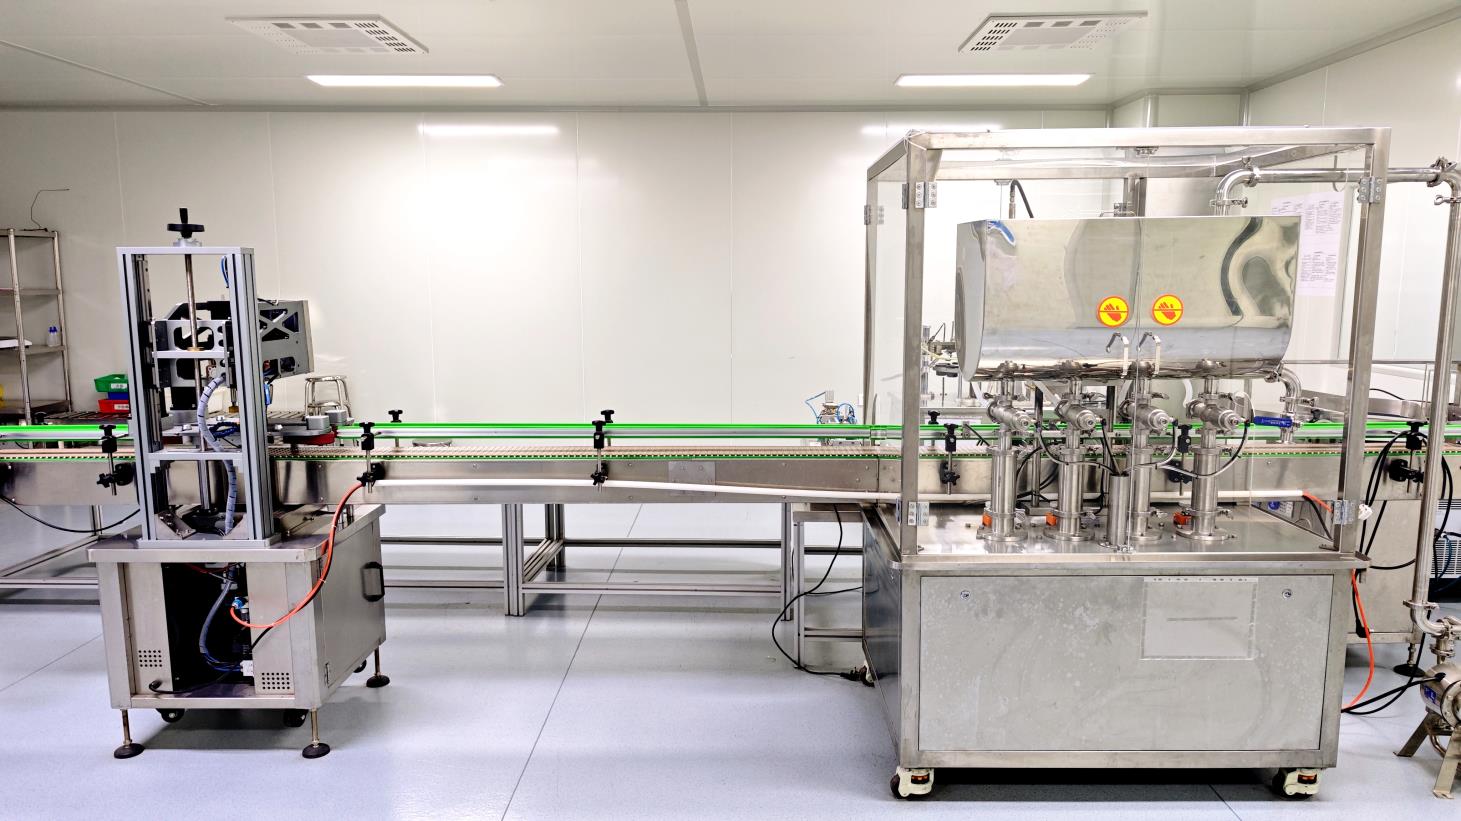
From initial polymer compound selection to multi-cavity injection molding, cleanroom extrusion, custom labeling, and terminal sterilization, ROA Medicare provides full-spectrum contract manufacturing services customized to client specifications. Our engineering framework eliminates supply chain fragmentation, guaranteeing absolute product consistency and regulatory compliance.
Our bio-engineering design team utilizes advanced Design for Manufacturability (DFM) protocols. We review 3D CAD models, evaluate fluid mechanics for respiratory and hemodialysis circuits, and rapid-prototype custom connectors, tubing wall thicknesses, and ergonomic structural braces.
We source ultra-pure medical-grade resins—including DEHP-free PVC, non-toxic TPE (Thermoplastic Elastomers), medical silicone, liquid-absorbent hydrocolloids, and polyurethane. Steel molds undergo micro-precision CNC machining for tight-tolerance medical components.
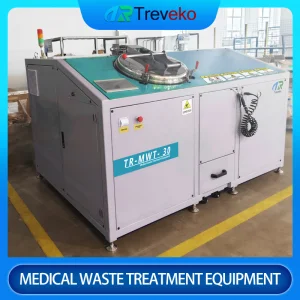
Manufacturing occurs in monitored ISO Class 7 and Class 8 cleanrooms. Depending on material sensitivity, we execute Ethylene Oxide (EtO) sterilization, Gamma Irradiation, or Automated Microwave Waste Infection Control treatments backed by full bio-burden test reports.
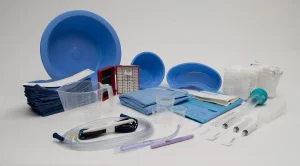
ROA Medicare maintains an expansive portfolio of specialized care solutions engineered for hospital intensive care units (ICUs), surgical theaters, homecare rehabilitation, and diagnostic pathology centers. Below is an engineering overview of our primary product clusters:
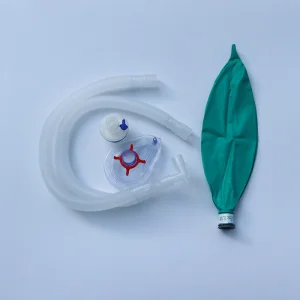
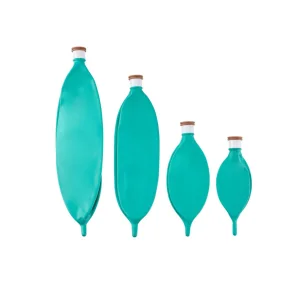
Our respiratory product division manufactures corrugated and smoothbore ventilator tubing circuits tailored for neonatal, pediatric, and adult intensive care. Available in standard lengths (1.2m, 1.5m, 1.8m, 2.0m), our circuits feature crush-resistant walls, minimal compliance values, and custom water trap integration. Complementary TPE breathing bags offer exceptional tactile sensitivity and complete latex-free safety.
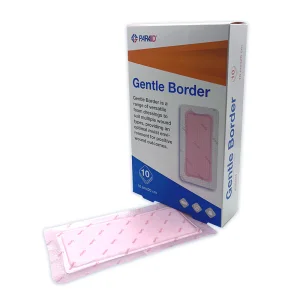
For chronic wound management and pressure ulcer prevention, we produce multi-layer waterproof adhesive silicone border foam dressings. Incorporating perforated soft silicone contact layers, super-absorbent core pads, and breathable polyurethane backing films, these dressings prevent tissue maceration while allowing pain-free atraumatic removal.
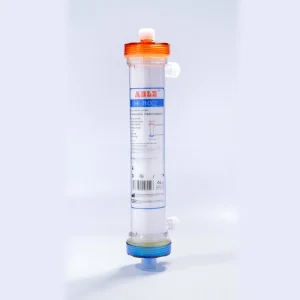
We engineer CE & ISO certified disposable hemodialyzer cartridges utilizing high-flux polyethersulfone (PES) synthetic membranes. Designed for optimal middle-molecule clearance, low albumin loss, and superior biocompatibility, these cartridges safeguard renal failure patients during acute and maintenance hemodialysis procedures.
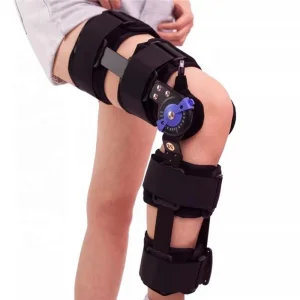
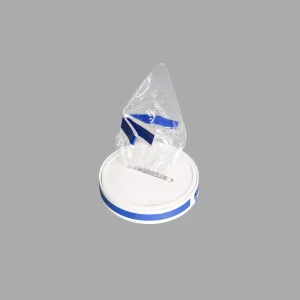
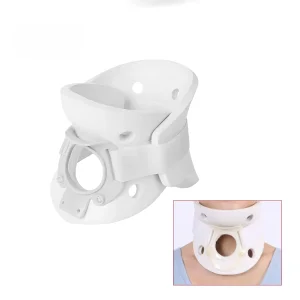
Our rehabilitation division produces post-operative knee braces with multi-angle dial hinges, casting tapes, and orthopedic splints. Furthermore, our surgical line supplies sports medicine suture anchor instrument sets and disposable latex-free endoscopic camera drapes to preserve sterile barriers during minimally invasive procedures.
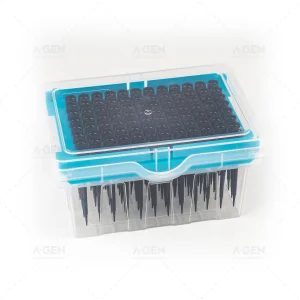
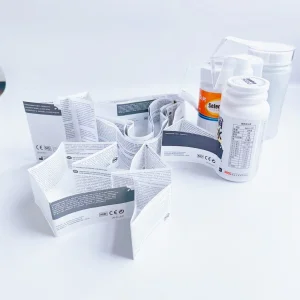
Supporting modern point-of-care testing (POCT) and laboratory automation, we supply conductive pipette tips compatible with Tecan LiHa systems (50µL capacity), rapid IVD blood testing kits, and bio-pharma standard packaging solutions with customizable OTC pharmaceutical vinyl labels.
To combat Healthcare-Associated Infections (HAIs), we offer 10% Povidone-Iodine disinfectants alongside integrated compact microwave sterilization machinery designed for localized, eco-friendly medical waste decontamination in small-to-medium clinical institutions.
Navigating regional healthcare regulations is critical for global distributors and medical OEMs. Hebei ROA Medicare Co., Ltd. integrates regulatory compliance directly into our Quality Management System (QMS).
Our facilities maintain full ISO 13485 certification for medical device design and manufacturing, ensuring every batch undergoes rigorous design history file (DHF) auditing, raw material inspection, and final lot release testing.
Products destined for the European Economic Area (EEA) are designed to satisfy European Medical Device Regulation (EU 2017/745) requirements, complete with technical documentation, risk assessment (ISO 14971), and post-market surveillance (PMS) protocols.
We provide full support for US FDA 510(k) submissions, DMF filings, and regional registration dossiers across Latin America, the Middle East, Southeast Asia, and Africa. Custom localized labeling, multi-lingual IFUs (Instructions for Use), and unique device identification (UDI) barcoding are standard offerings.
As medical technology evolves toward digital connectivity, eco-friendly materials, and decentralized patient care, ROA Medicare is committed to pioneering strategic technical advancements.
Get quick answers to common questions regarding our OEM contract manufacturing, quality certifications, minimum order quantities (MOQs), and global delivery capabilities.
Standard OEM development timelines range from 4 to 8 weeks depending on product complexity. This includes initial 3D design evaluation, mold manufacturing, prototype sampling, bio-compatibility testing, and pilot run approval. Accelerated prototyping options are available upon request.
Yes. All single-use patient care products—including our neonatal ventilator tubing circuits, TPE breathing bags, and wound dressings—are manufactured using 100% latex-free, non-toxic, medical-grade materials tested according to ISO 10993 cytotoxicity and sensitization standards.
Absoltely. Our in-house regulatory affairs team provides comprehensive technical dossiers (STED), Certificates of Free Sale (CFS), ISO 13485 audit reports, CE Declarations of Conformity, and sterilization validation data to facilitate seamless registration with your national health ministry.
MOQs vary by product category. Standard medical disposables usually require 5,000 to 10,000 units for fully customized private label artwork, box printing, and pouch sterilization. However, we offer flexible tier structures for initial market evaluation trials.
We enforce automated statistical process control (SPC) throughout cleanroom extrusions and molding. Every finished lot undergoes randomized physical tolerance testing, leak-rate verification, sterile barrier testing, and micro-particle analysis prior to warehouse release.
Browse our extended range of specialized surgical tools, hemodialysis systems, POCT consumables, and advanced homecare products.

 ROA Medicare